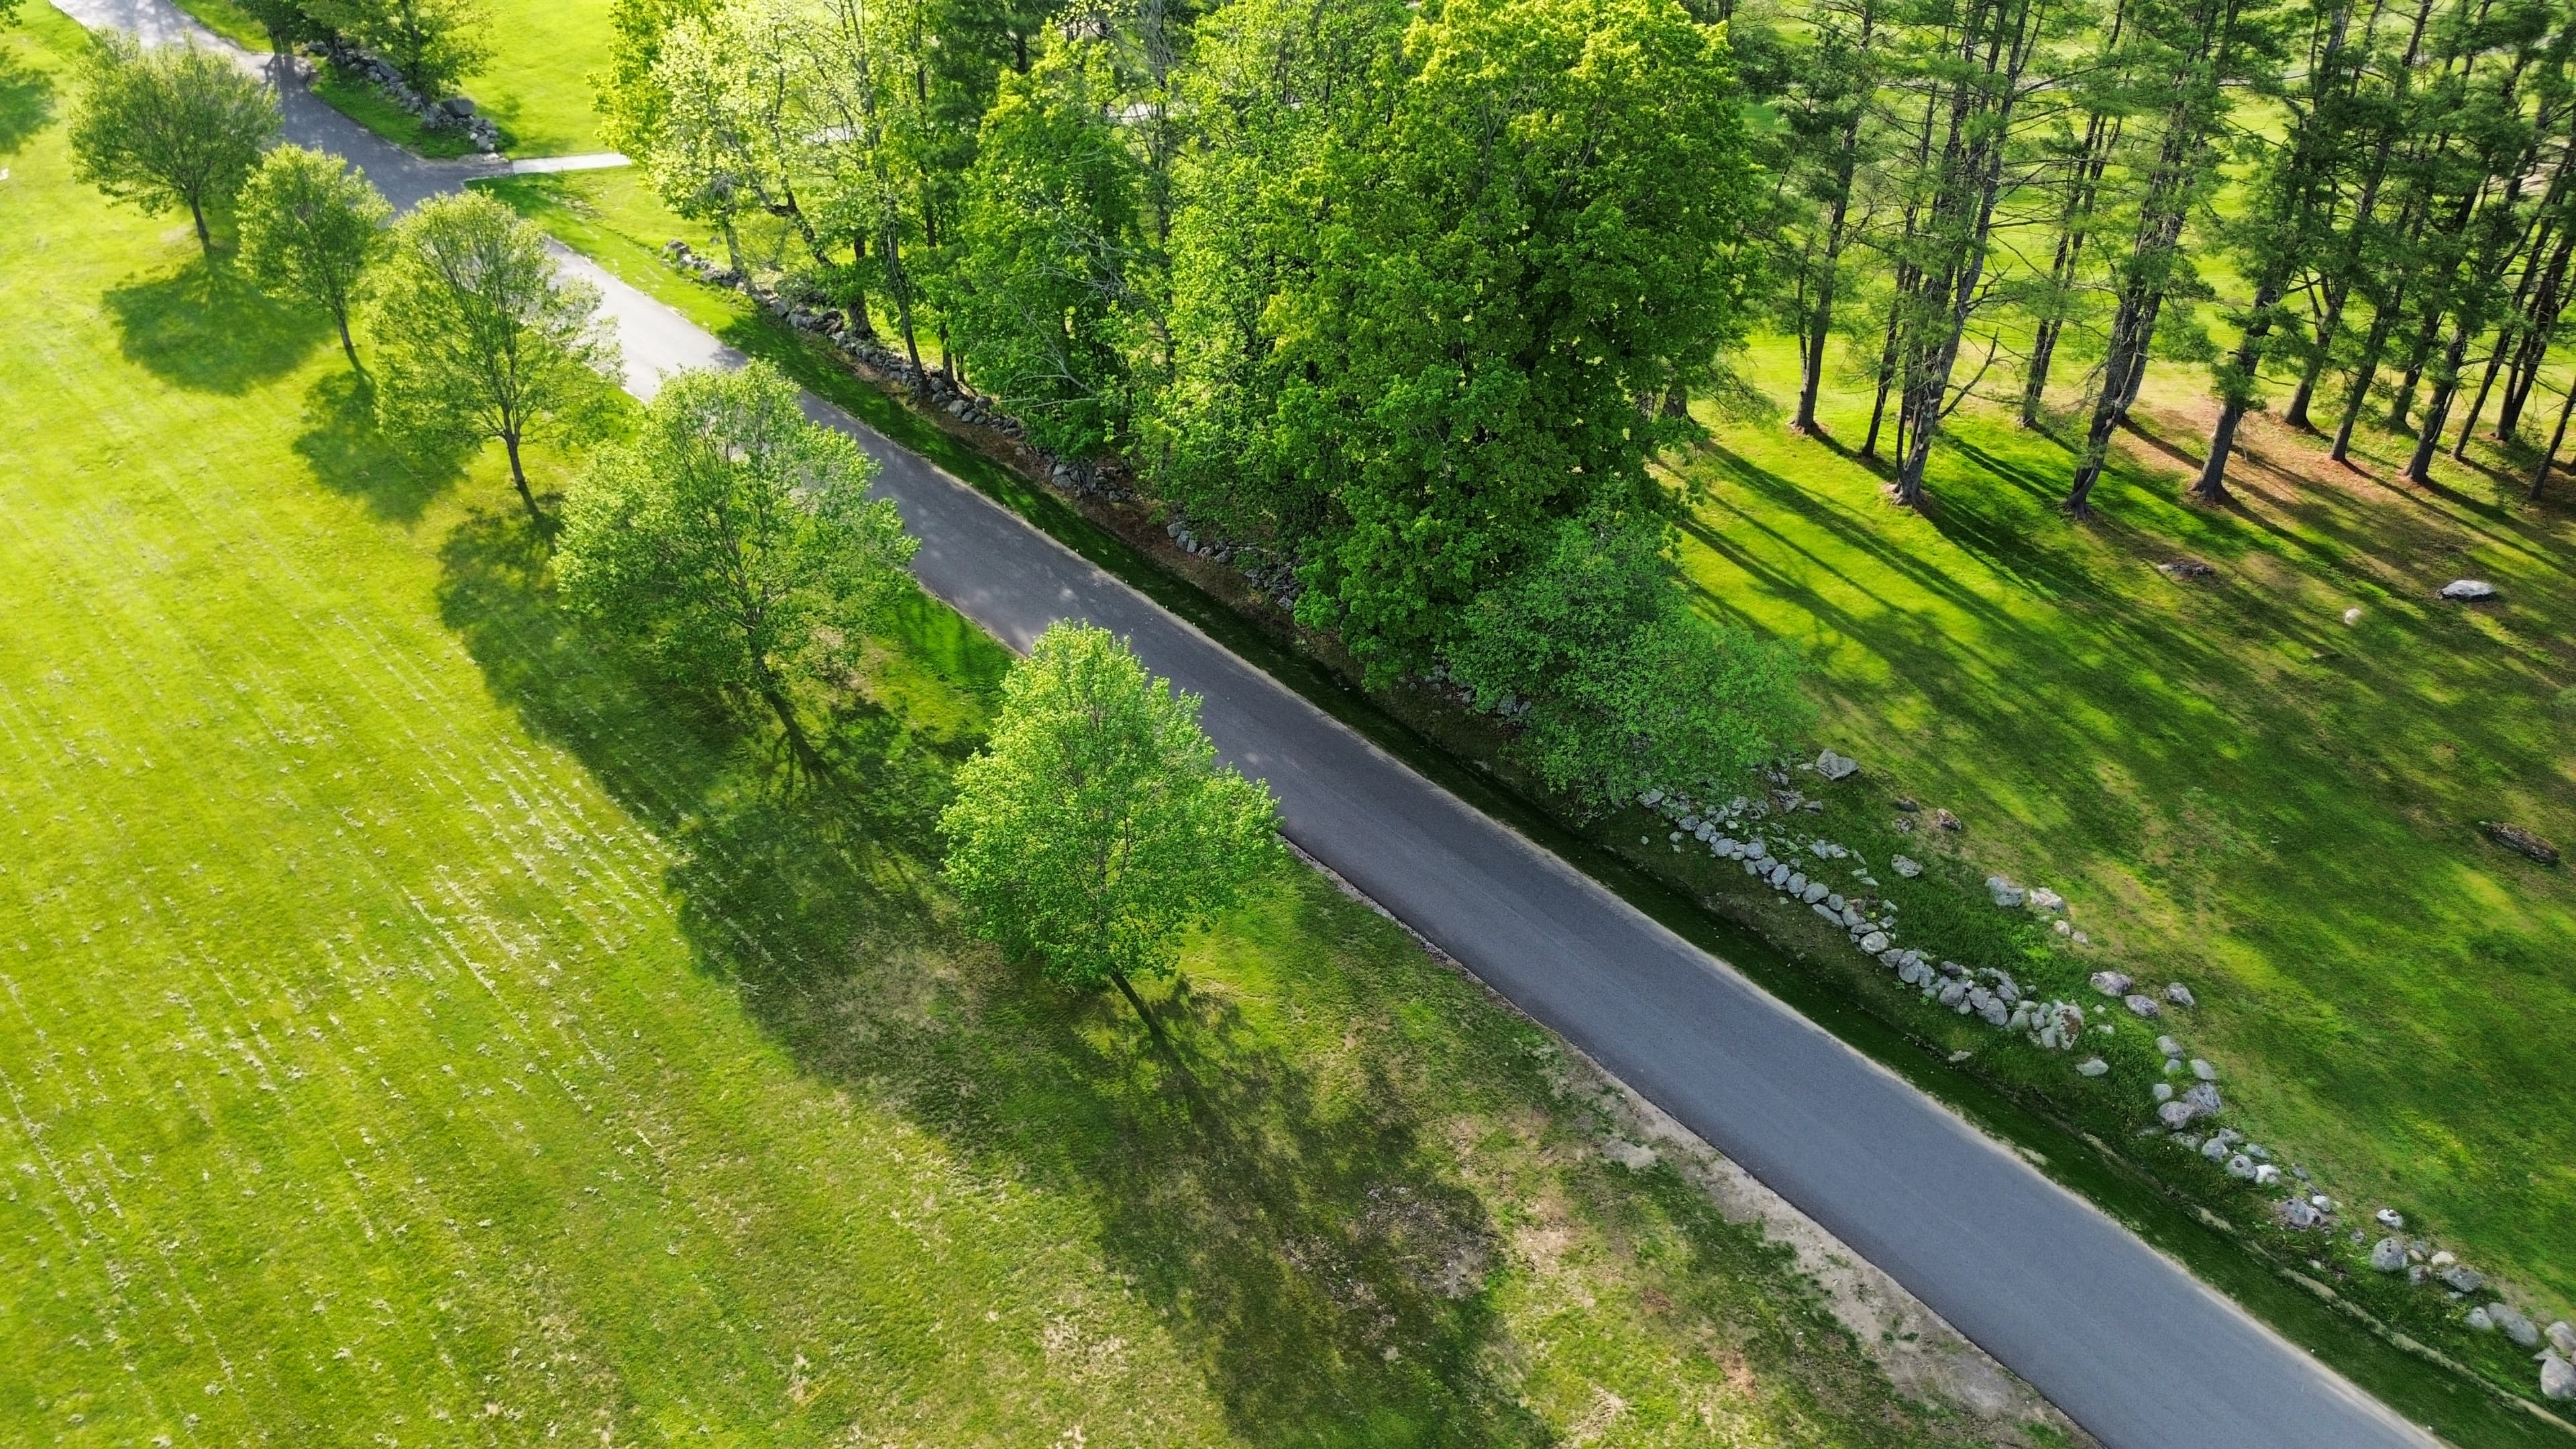
Crowne Point Country Club Case Study
Crowne Point Country Club rehabilitated a deteriorated Vermont access road with MIRAFI H2Ri, using active moisture management to address saturated soils, frost-related distress and subgrade instability.
>


Deployment of double-sided textured GSE® HD FrictionFlex geomembrane for the new tailings pond at the Umm Wu’al Phosphate Project in Saudi Arabia.

Installation of FABRINET drainage composite as a drainage layer below the GSE® HD FrictionFlex geomembrane liner.

Installing high-performance geomembrane for secure toxic tailings containment at Umm Wu’al Phosphate Project, Saudi Arabia.
Crowne Point Country Club Case Study
Crowne Point Country Club rehabilitated a deteriorated Vermont access road with MIRAFI H2Ri, using active moisture management to address saturated soils, frost-related distress and subgrade instability.

Lake bank stabilization at Vivid Shores
At Vivid Shores in Bonita Springs, Florida, PROPEX® Armormax®, MIRAFI® FW403 and MIRAFI 140N stabilize lake banks exposed to wind-driven wave erosion. Completed sections are performing as designed.

When Traditional Sand Bunds Fail: A GEOTUBE Marine Solution for Land Reclamation
When traditional sand bund construction failed on an extremely soft marine clay seabed, GEOTUBE® Marine systems provided a stable containment solution that helped advance a land reclamation project for 112 acres.
The Umm Wu’al Phosphate Project in the Kingdom of Saudi Arabia is a large-scale mining and processing operation launched in 2014 by Maaden Phosphate Company, a joint venture with SABIC, aimed to establish a world-class, fully integrated phosphoric fertilizer production facility. With the project continually expanding, additional infrastructure was required to safely manage highly toxic tailings. The construction of new tailings ponds was essential to ensure that waste streams were securely contained and did not pose a risk to the surrounding environment.
The expansion of the Umm Wu’al Phosphate Project required a new tailings pond to contain highly toxic by-products of fertilizer production. Containment integrity was non-negotiable, as any seepage could have significant environmental and operational consequences. Key challenges for this phase of the project included:
Supplying extremely large volumes of geomembrane within demanding delivery timeframes.
Meeting strict requirements for geomembrane flatness and smoothness to ensure consistent installation performance in the very hot climate of Saudi Arabia.
Maintaining a standard of 100 percent flawless material, with no leaks or defects permitted.
These requirements were reinforced by the experience of the first project phase in where Solmax supplied 1.4 million m2 of double-sided GSE® HD FrictionFlex geomembrane and 550,000 m2 of FABRINET® geocomposite. The performance of this first installation set the benchmark for quality and reliability. For phase two, strict protocols were established to ensure identical outcomes.
Solmax’s role was to deliver the 900,000 m2 of GSE HD FrictionFlex geomembrane required for the second phase of the tailings pond construction. GSE HD FrictionFlex, a double-sided textured geomembrane, was chosen for its ability to provide high interface friction angles, stability on slopes, and durability under extreme environmental conditions. To meet the requirement for flawless material, Solmax implemented a comprehensive quality assurance process. This began with stringent pre-selection criteria and continued through in-factory production monitoring. Maaden’s engineering representatives sampled and tested the geomembrane during production, ensuring conformance to all specifications. Two independent inspectors were present in the manufacturing plant 24 hours a day. Their responsibilities included supervising material production and storage, monitoring quality control procedures, and witnessing laboratory testing. Spark testing was conducted to confirm that the geomembrane was free from leaks or flaws, while additional sampling was sent to external laboratories for verification.
This rigorous process guaranteed that only flawless material was shipped to site. The quality assurance procedures, combined with Solmax’s manufacturing capacity and supply chain coordination, enabled all materials to be produced, tested, and delivered on schedule. Despite the scale of the order and the harsh environmental conditions of Saudi Arabia, Solmax successfully met all project requirements.
The result was a fully lined tailings pond capable of safely containing toxic process waste. The supply and quality assurance program reinforced Solmax’s reputation as a trusted partner for large-scale mining and industrial projects where containment performance is critical.