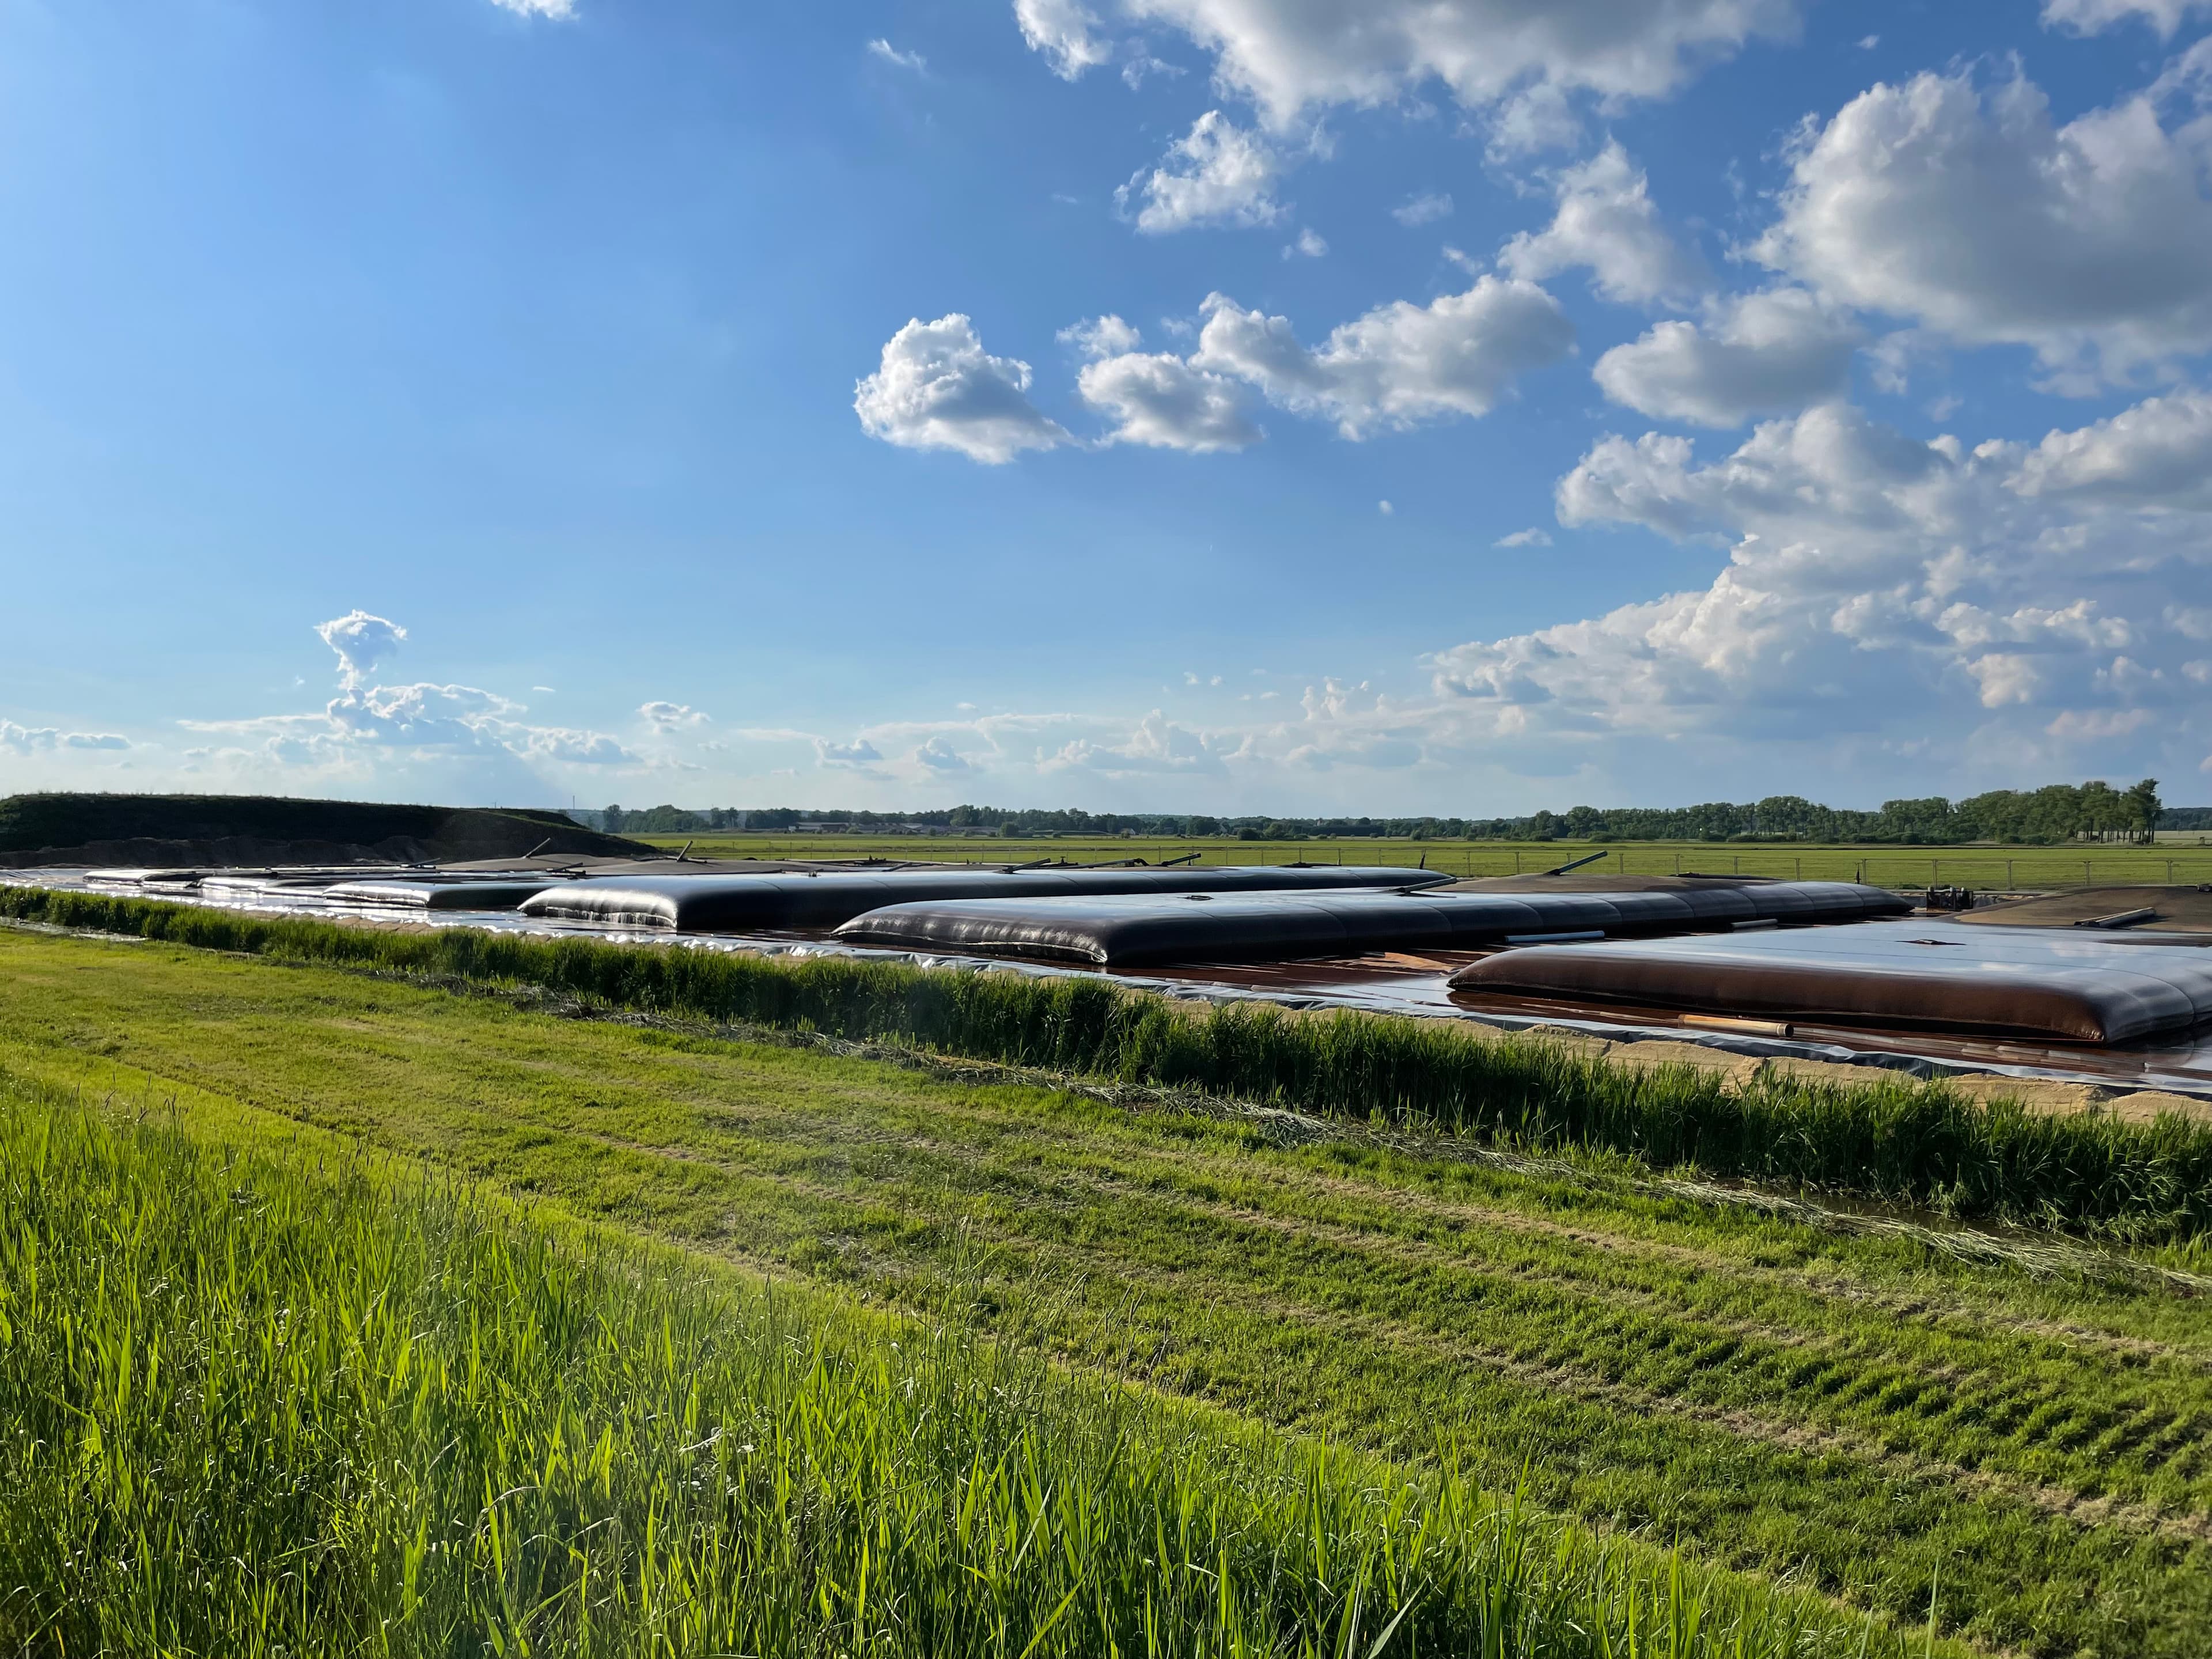
Dredging the Schwarze Elster River with GEOTUBE
Discover how GEOTUBE® dewatering systems helped manage 10,000 m³ of sediment from the Schwarze Elster River, delivering an effective dewatering, containment and cost-effective solution.
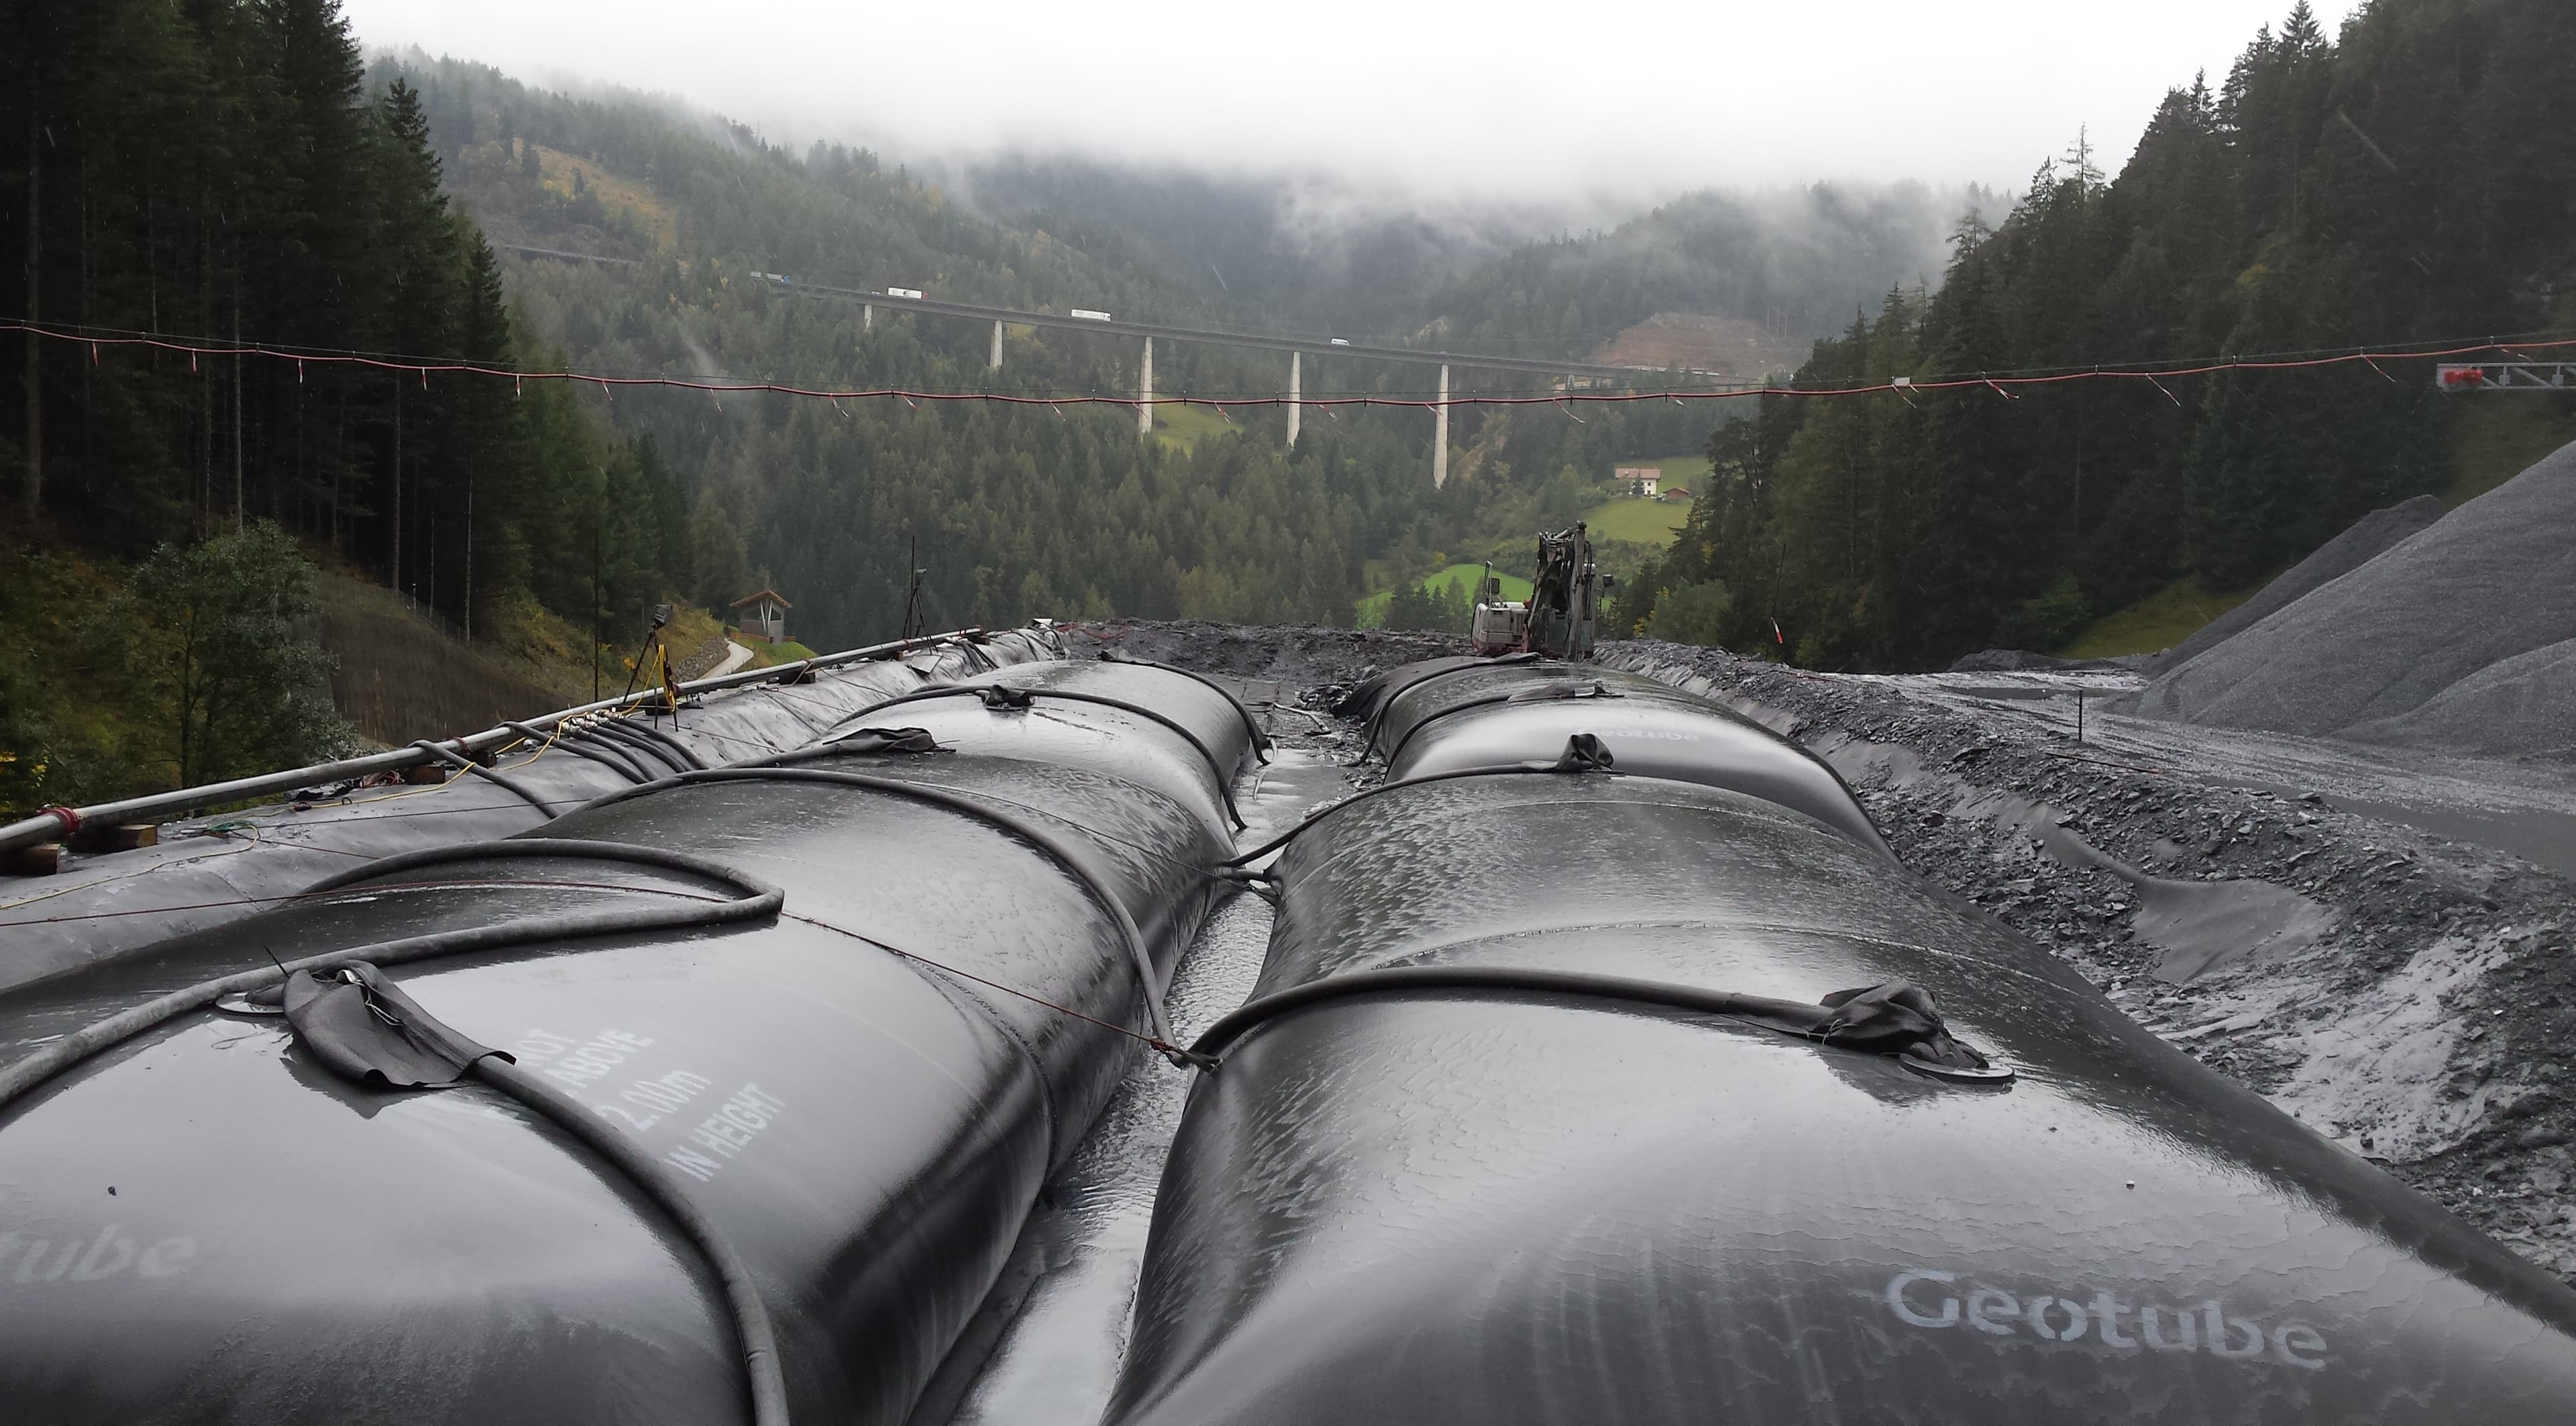
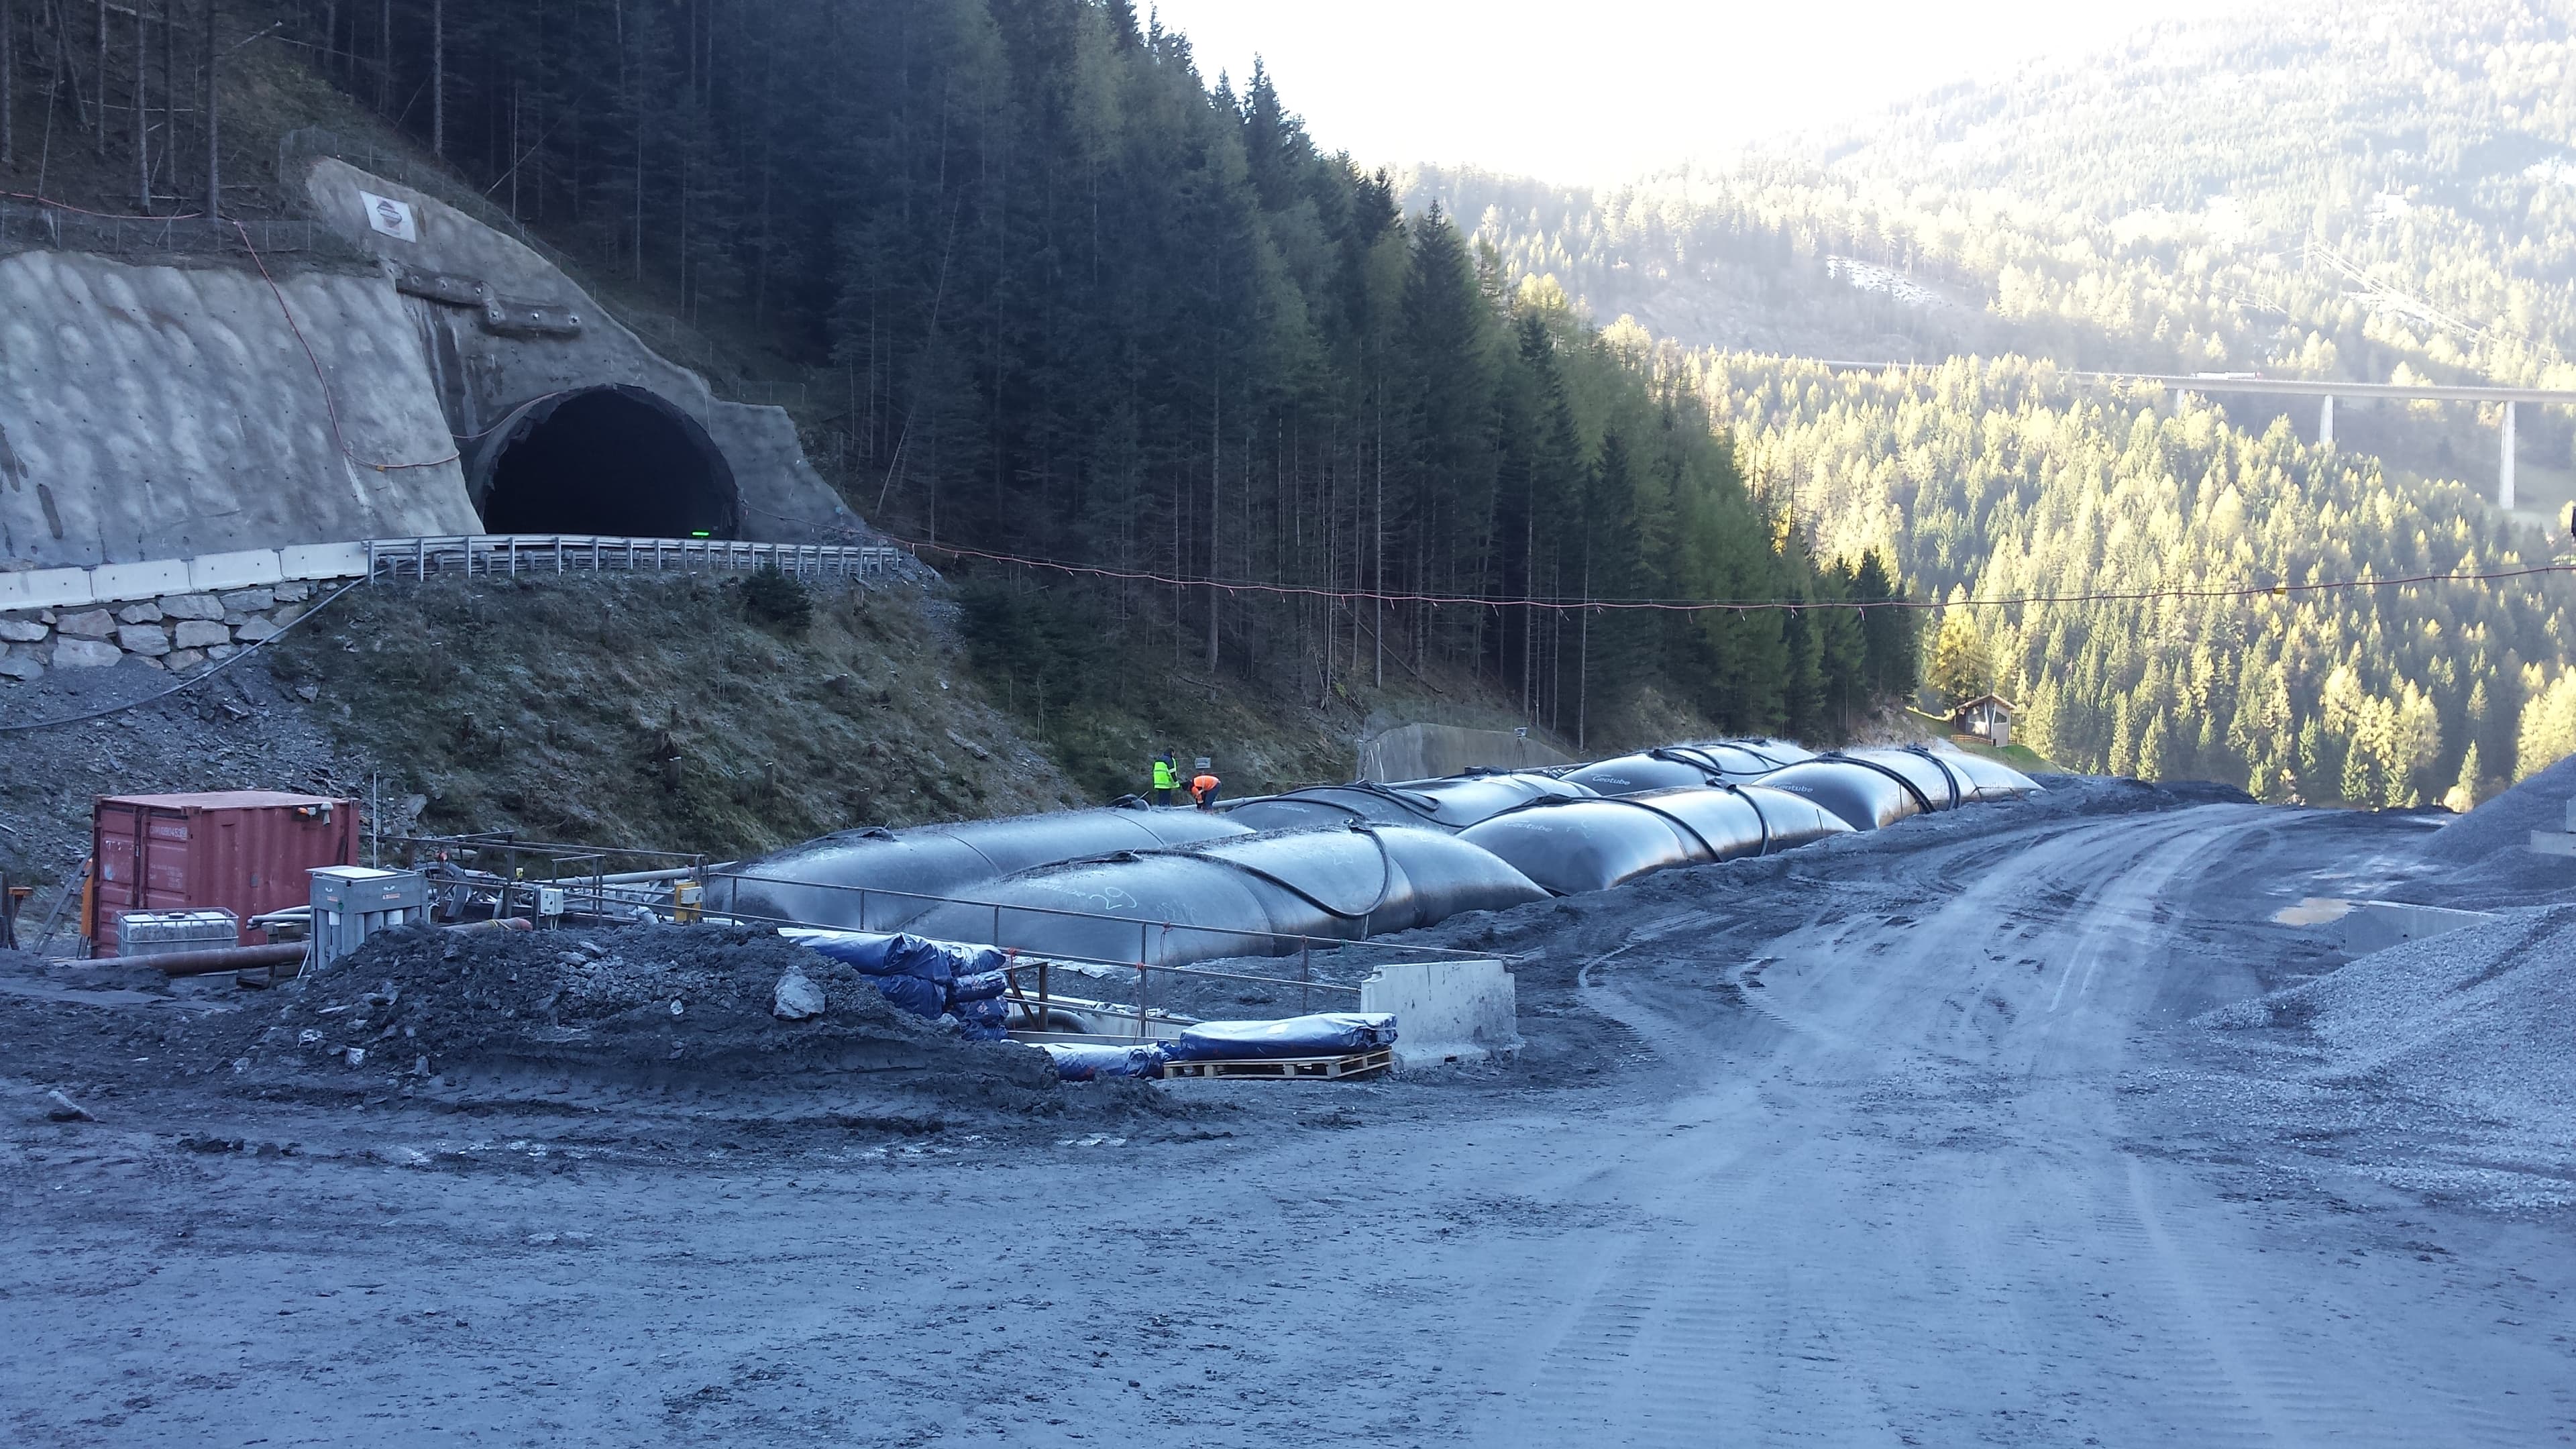
A compact GEOTUBE® dewatering setup was installed on a 45 × 10 m field, using a rotating arrangement of three tube pairs to allow continuous sludge treatment during aggregate washing operations.
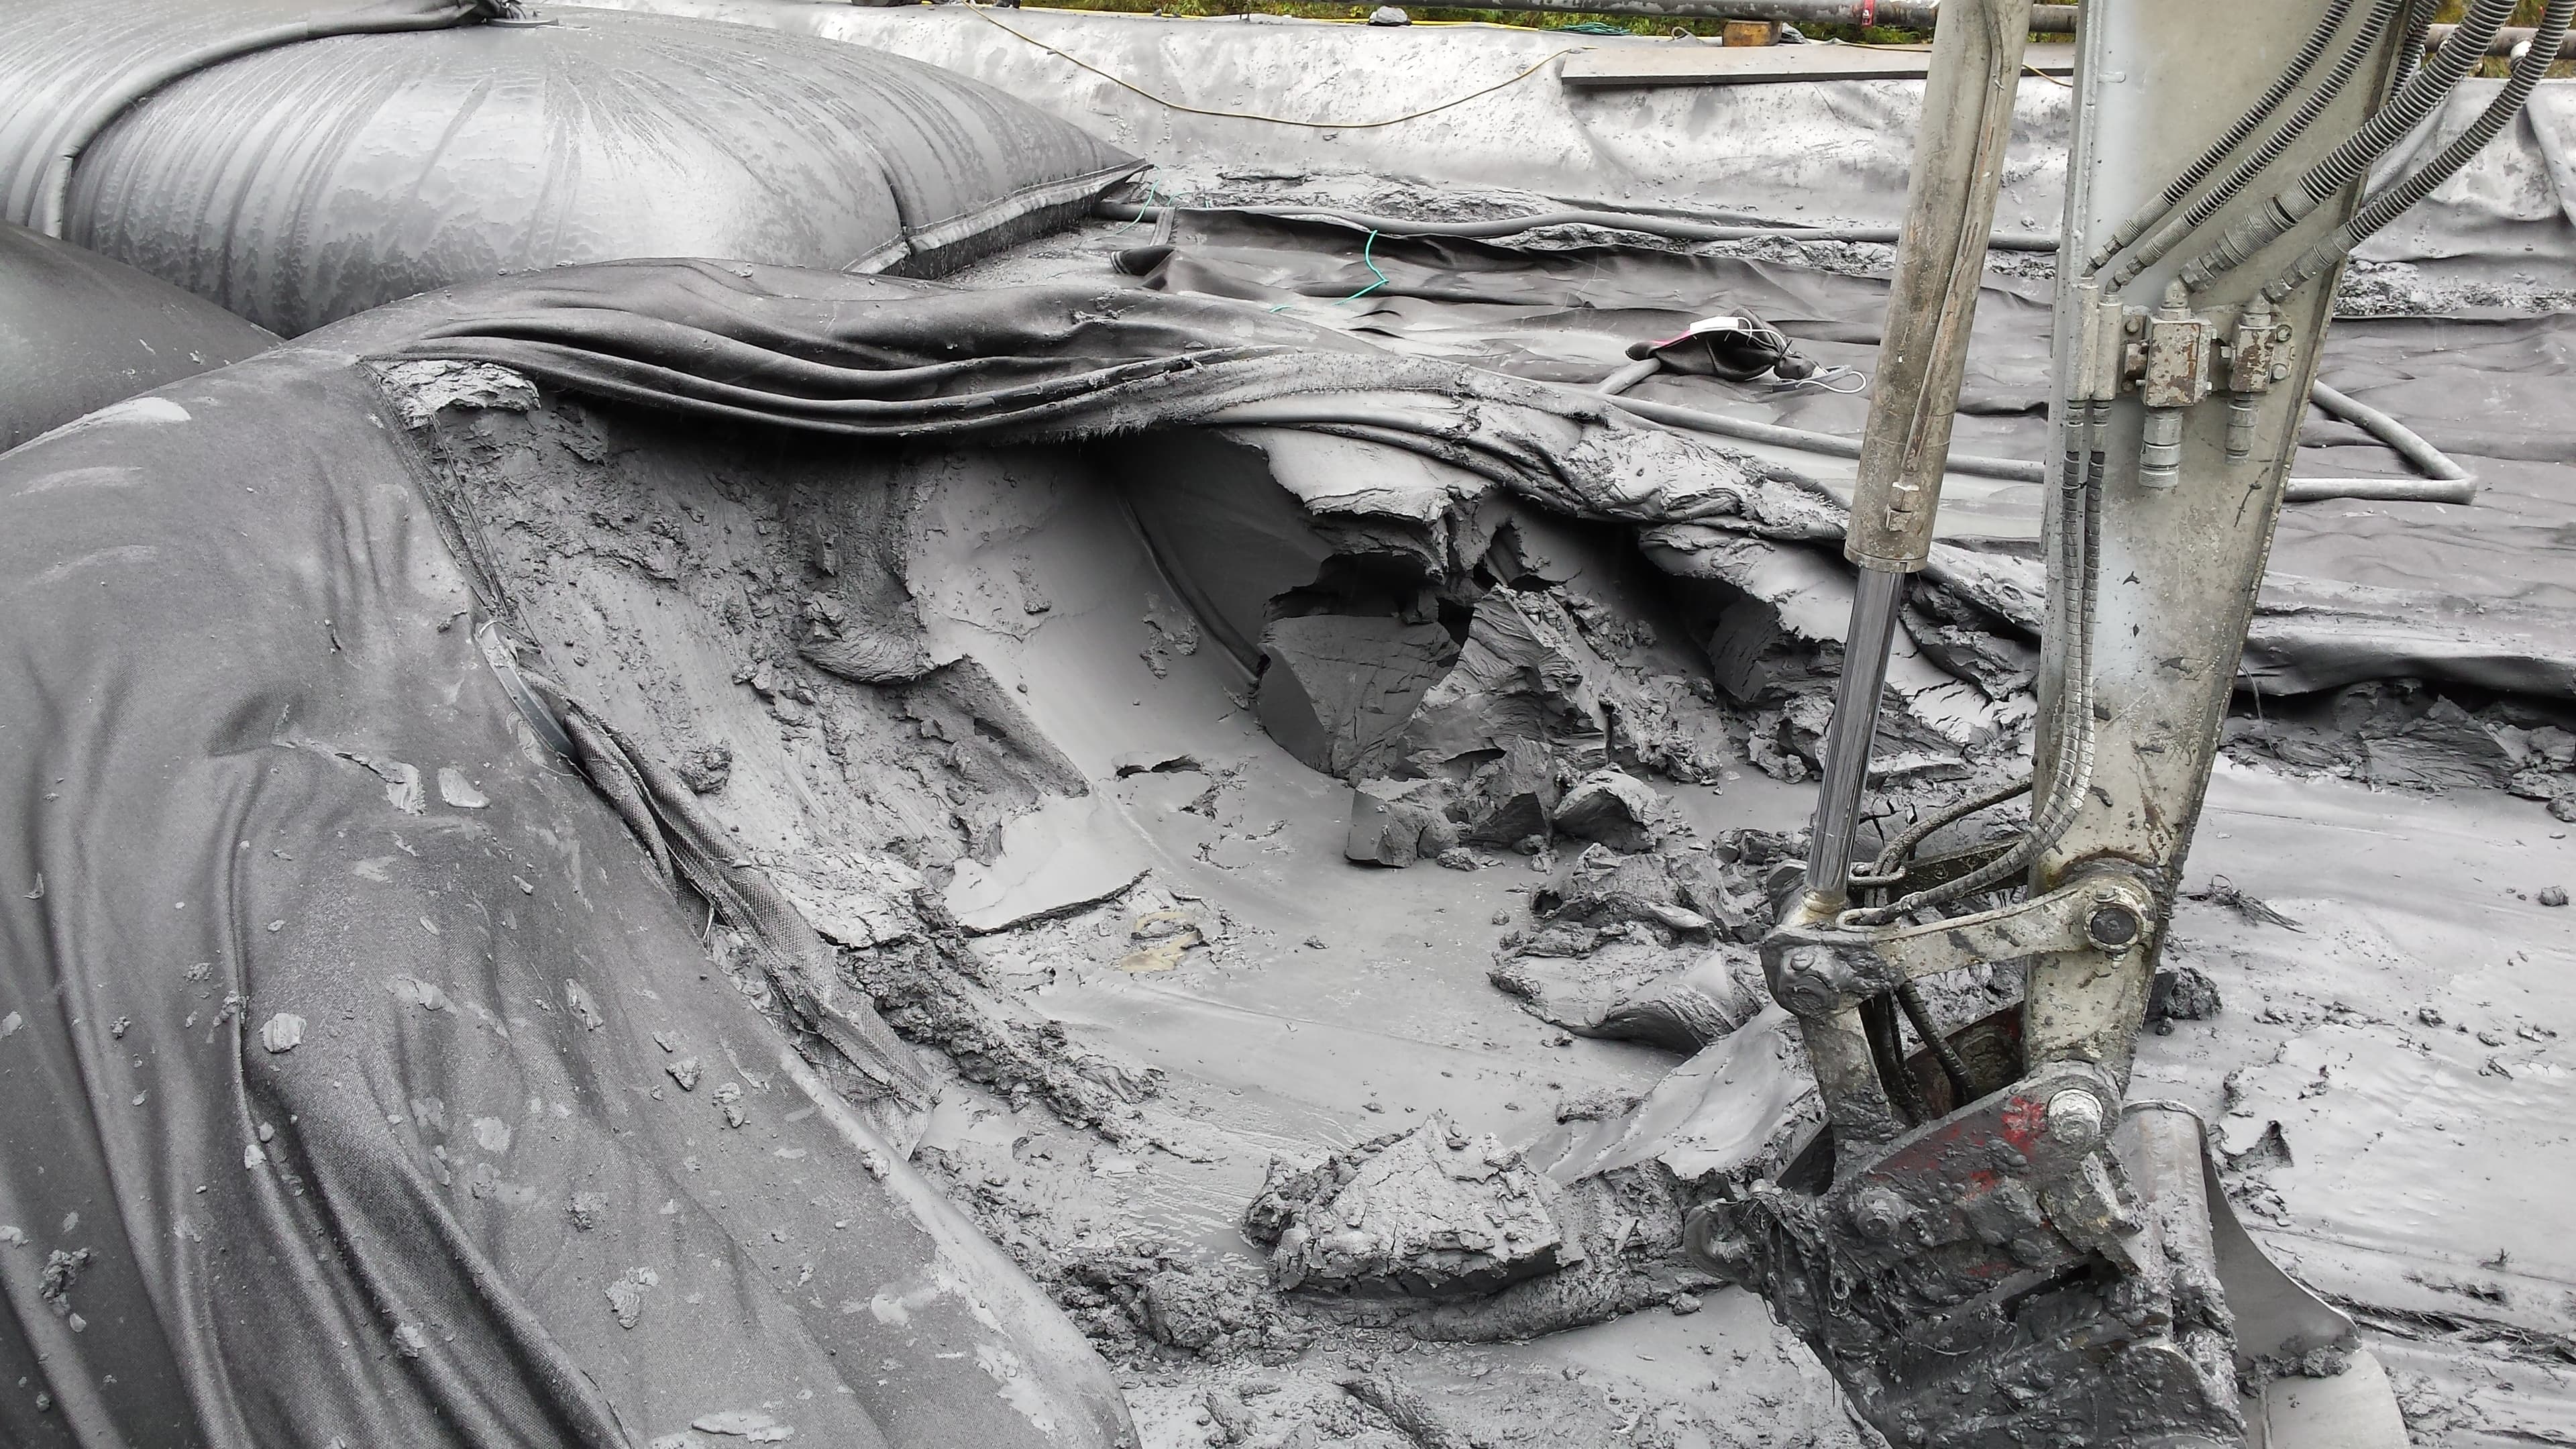
Each dewatering tube was designed to contain approximately 350 m³ of sludge, enabling flexible handling of fluctuating slurry volumes and dry solids content.
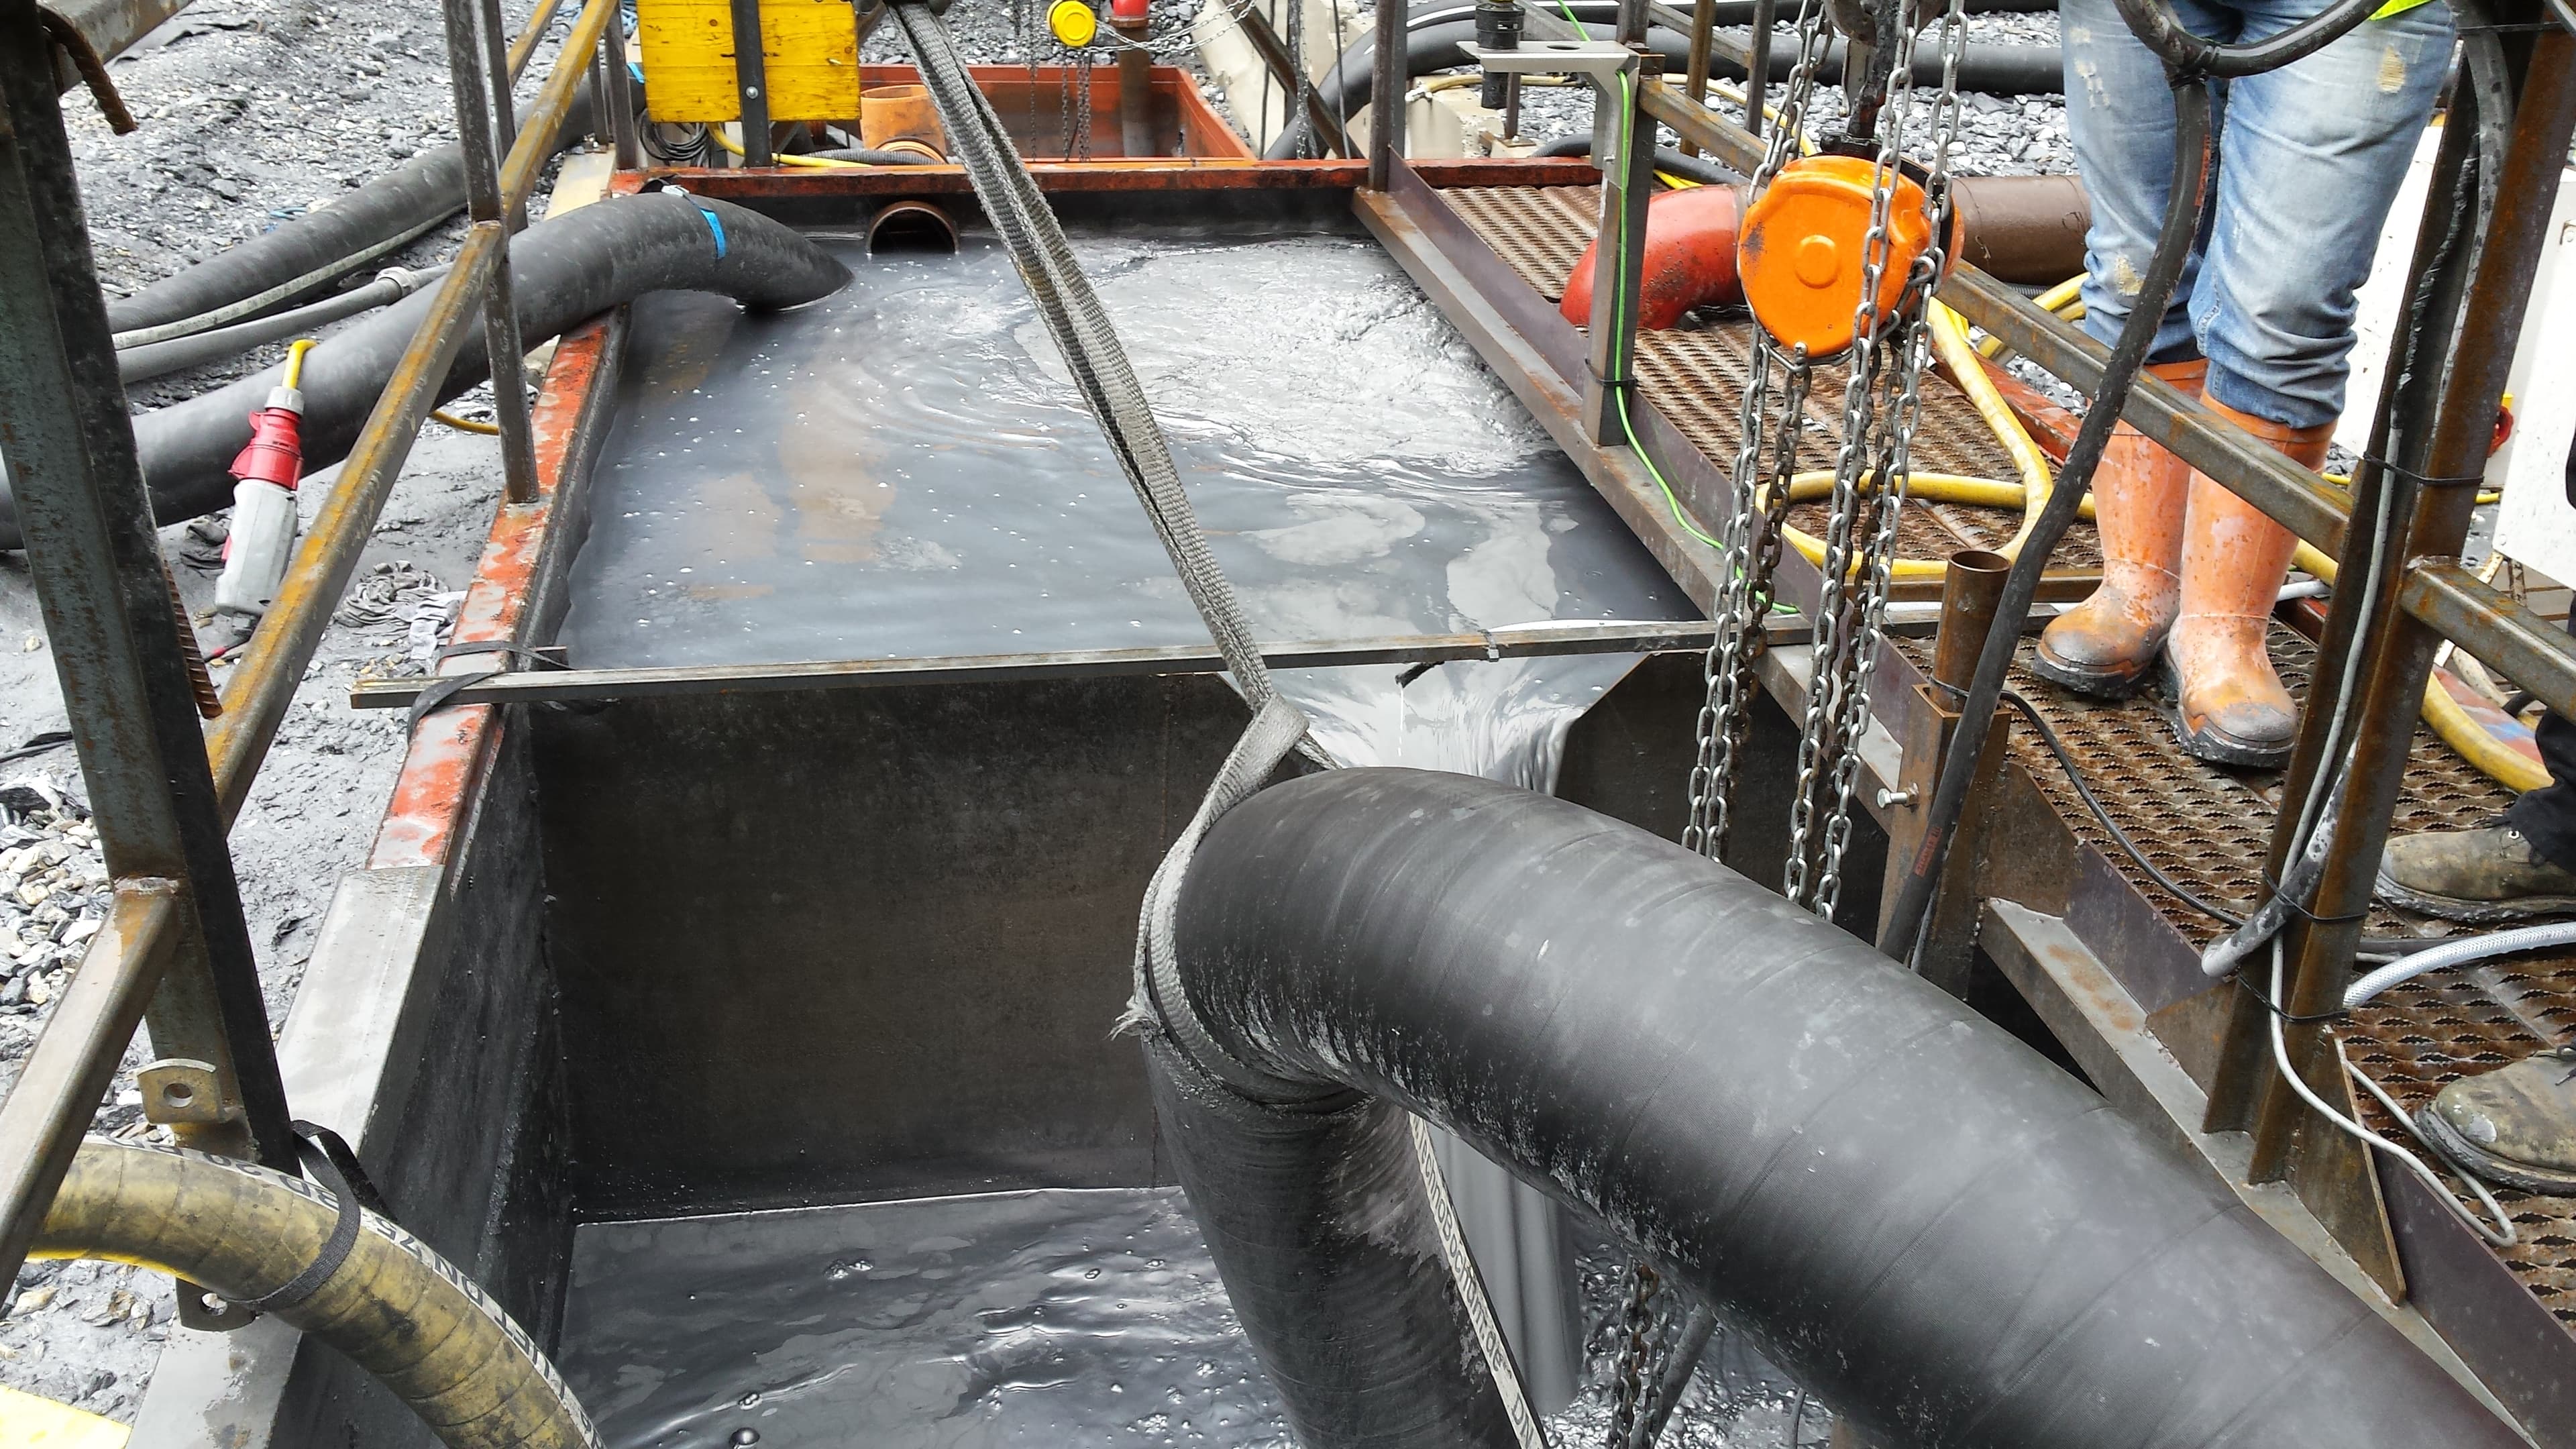
Clarified effluent discharged from the GEOTUBE® units was pumped back to the wash plant for immediate reuse, while the dewatered material was excavated and transported to the deposit area using standard earthmoving equipment.
Dredging the Schwarze Elster River with GEOTUBE
Discover how GEOTUBE® dewatering systems helped manage 10,000 m³ of sediment from the Schwarze Elster River, delivering an effective dewatering, containment and cost-effective solution.
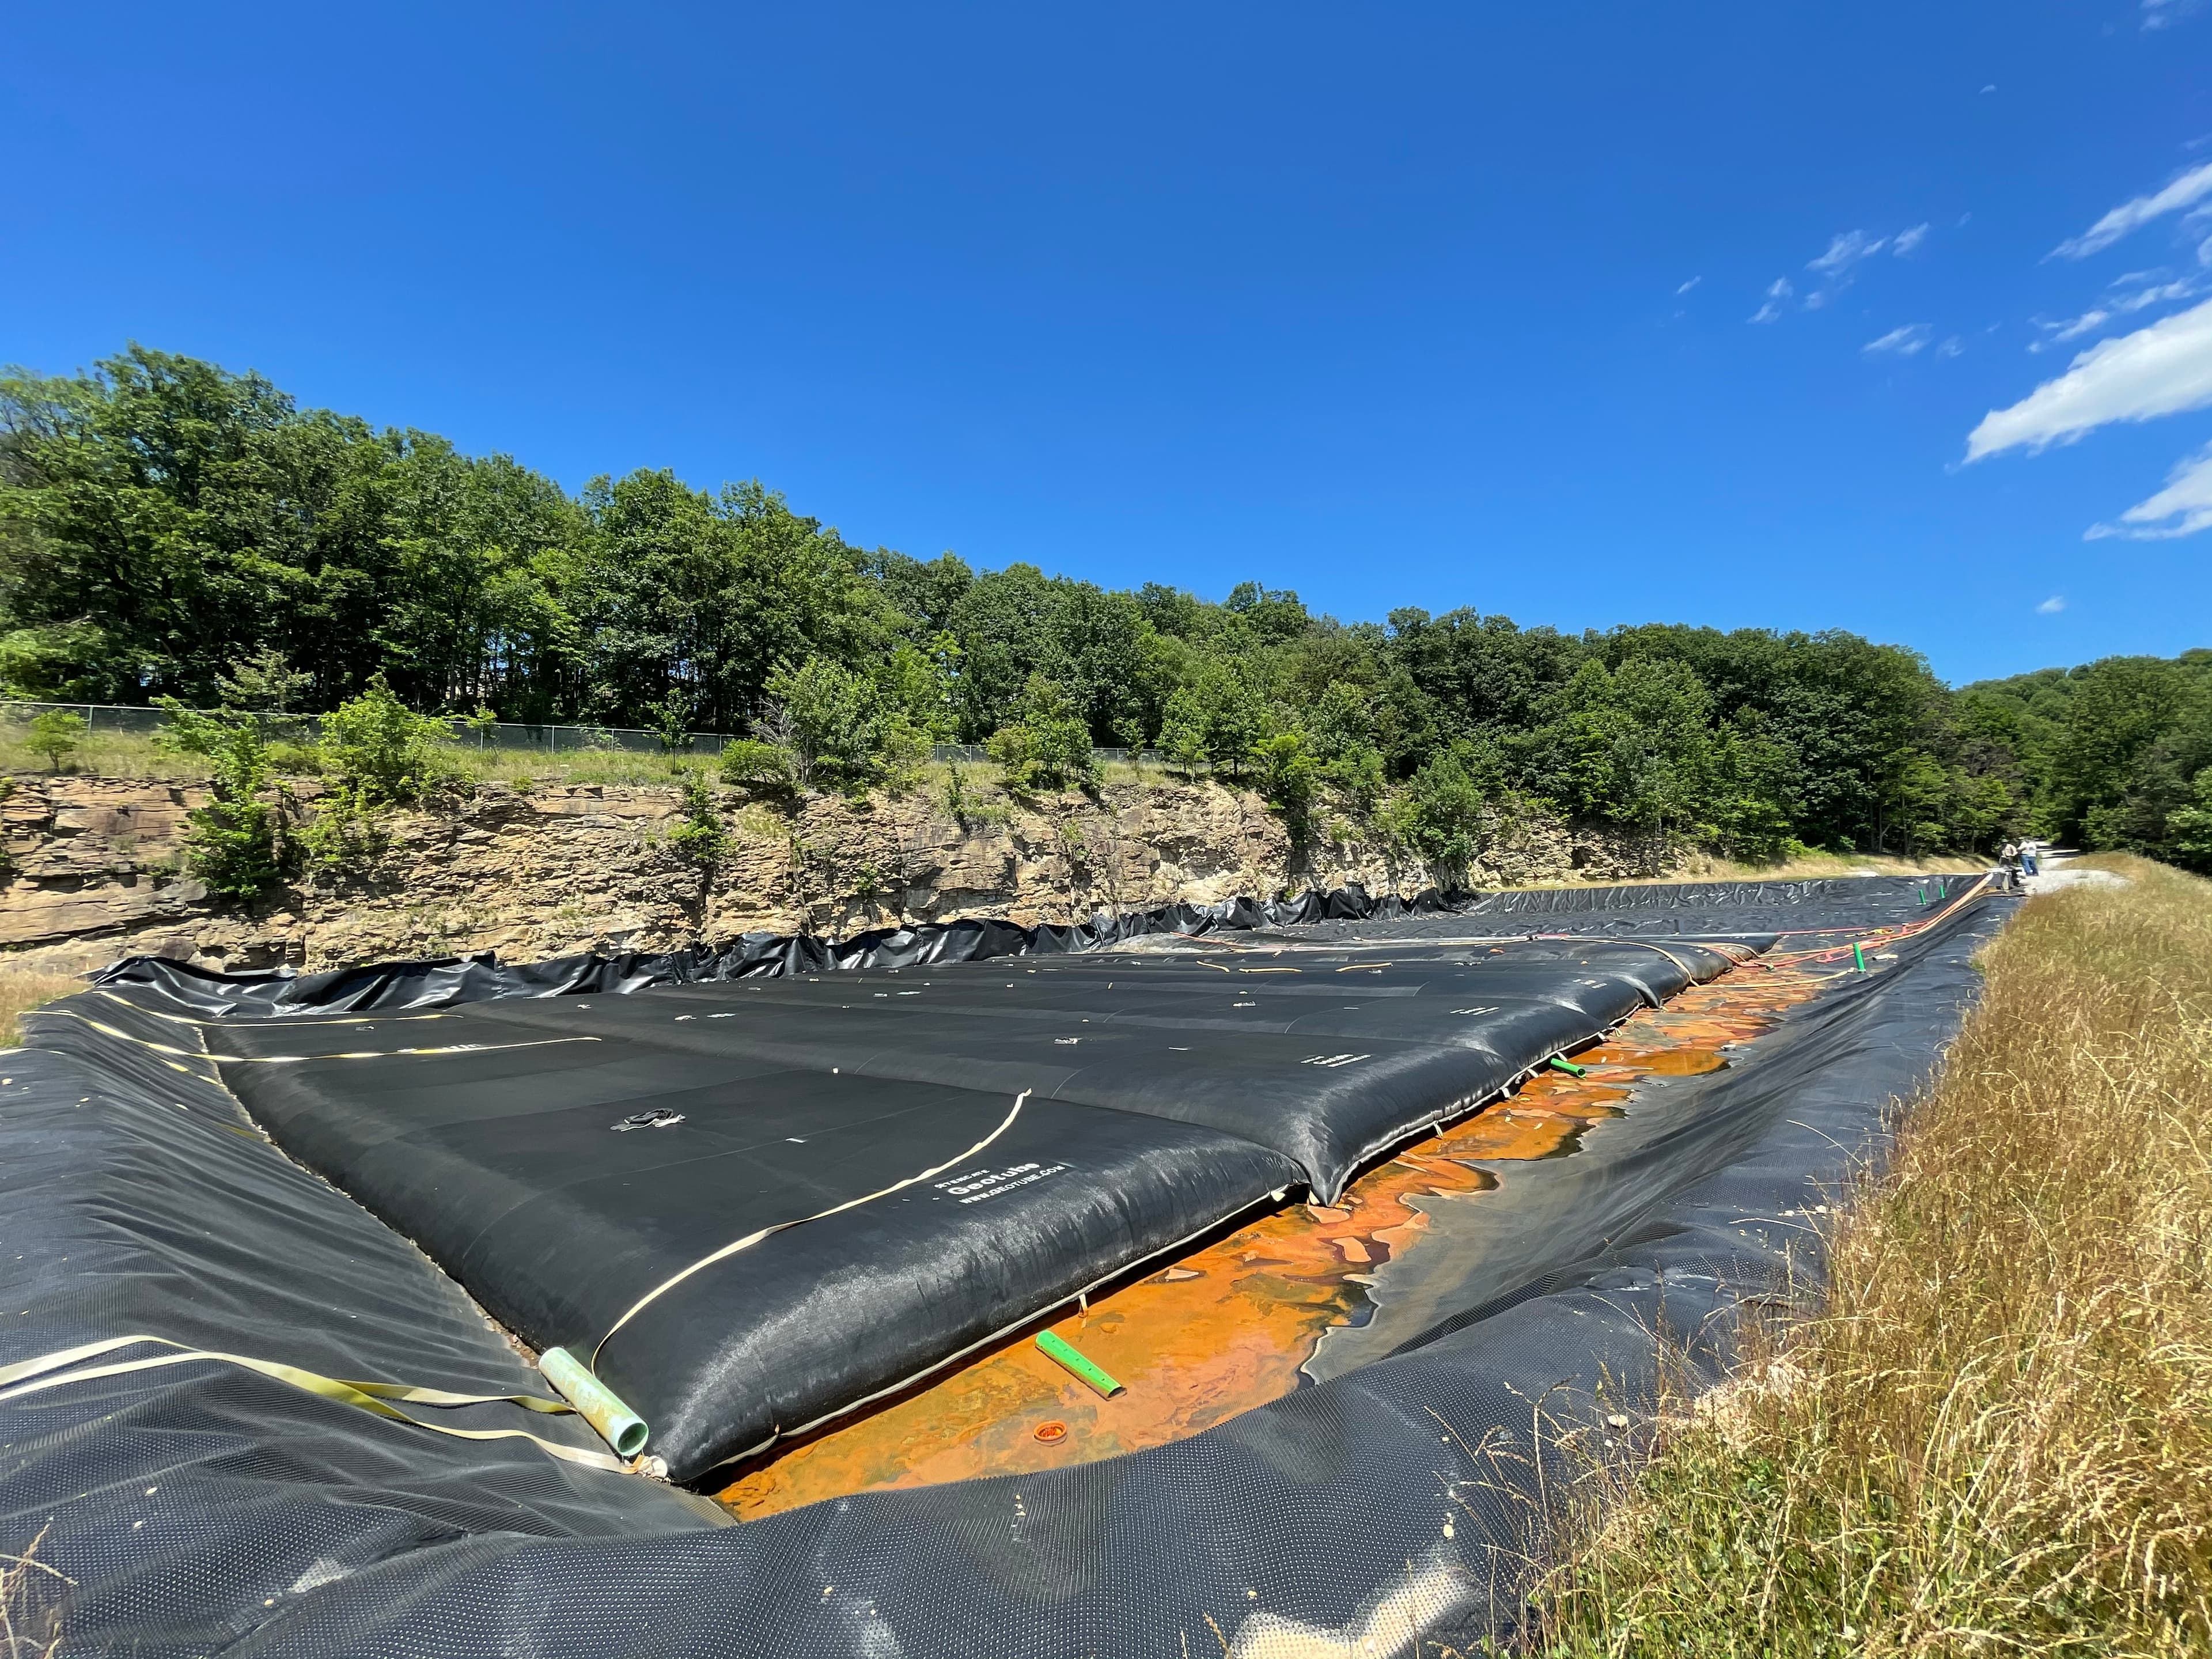
Omega Mine extends AMD treatment capacity with dewatering
At Omega Mine in West Virginia, GEOTUBE® GT500 units help the West Virginia Department of Environmental Protection treat and dewater acid mine drainage from abandoned mines while supporting long-term capacity and compliance.

Dredging and reuse of contaminated sediments
Embraport used dewatered contaminated sediments as structural fill within its terminal platform, saving 400,000 m3 of imported material and reducing earthfill platform costs by 20% to 30%.
Large-scale tunnelling along the Scandinavian–Mediterranean TEN corridor generated significant volumes of excavated material that required grading and washing for reuse in concrete and fill applications. At the Wolf access gallery, the wash plant processed bored aggregates, recovering approximately 30 percent of the material for beneficial reuse. The finest fraction, however, retained most of the water and produced a voluminous slurry. Because resource efficiency was a core requirement of the project, wash water had to be reused in a closed loop. This made reliable solids removal essential at the end of each washing cycle. Any disruption to water quality or availability directly threatens the continuity of daily operations.
The grading process produced slurry with a higher than expected and highly variable solids content. Fluctuations in dry solids and inconsistent slurry output placed strain on conventional mechanical treatment systems. These systems typically require high capital investment, consume significant energy, and are sensitive to changes in feed conditions. Space constraints at the construction site further limited available options, while maintenance interruptions and downtime risked halting aggregate production entirely. The treatment solution therefore needed to respond flexibly to changing slurry characteristics, deliver consistently clear effluent suitable for immediate reuse, and produce dewatered sediments stable enough for road transport, all at the lowest possible operational cost.
To address these constraints, the contractor adopted tube dewatering using GEOTUBE® units. After comparative trials, the GEOTUBE GT500D geotextile fabric was selected due to its superior effluent clarity and sustained permeability under fluctuating solids loads. With technical support, a rotating system of three pairs of tubes was established on a compact footprint of approximately 45 × 10 m. Each GEOTUBE dewatering containers accommodated about 350 m³ of sludge, allowing continuous operation by alternating filling and dewatering cycles.
Prior to entering the GEOTUBE dewatering containers, the slurry was mixed with inline injection of polymers. This treatment agglomerated fine particles into larger flocs, accelerating dewatering and preserving the permeability of the geotextile. Clarified effluent discharged from the tubes was pumped directly back to the wash plant, maintaining an uninterrupted water supply. The dewatered solids were reduced to roughly 10 percent of the original slurry volume and could be handled using the same excavators employed in daily grading operations. Dewatered material was then transported by truck to the deposit area in a clean and controlled manner.
This approach delivered a flexible, low-energy dewatering system that accommodated variable slurry conditions, ensured high-quality water reuse, and supported continuous aggregate processing within the spatial and operational limits of the tunnelling works.